


Gear hobbing is one of the most common methods for producing external spur and helical gears in volume. It is widely used across automotive, industrial machinery, and power tool applications where production quantities justify the tooling cost.
A rotating cutting tool called a hob cuts gear teeth into a blank in continuous motion. The process is fast, precise, and economical for high volumes. A single hob can cut gears with different tooth counts as long as the module is the same.
Hobbing is not the answer for every gear. Some gear types and precision requirements require other manufacturing methods.
This article explains what gear hobbing is, how it works, its advantages and limitations, and where it fits in gear manufacturing. It also compares hobbing with other methods and covers common problems and practical solutions.
1. What Is Gear Hobbing?
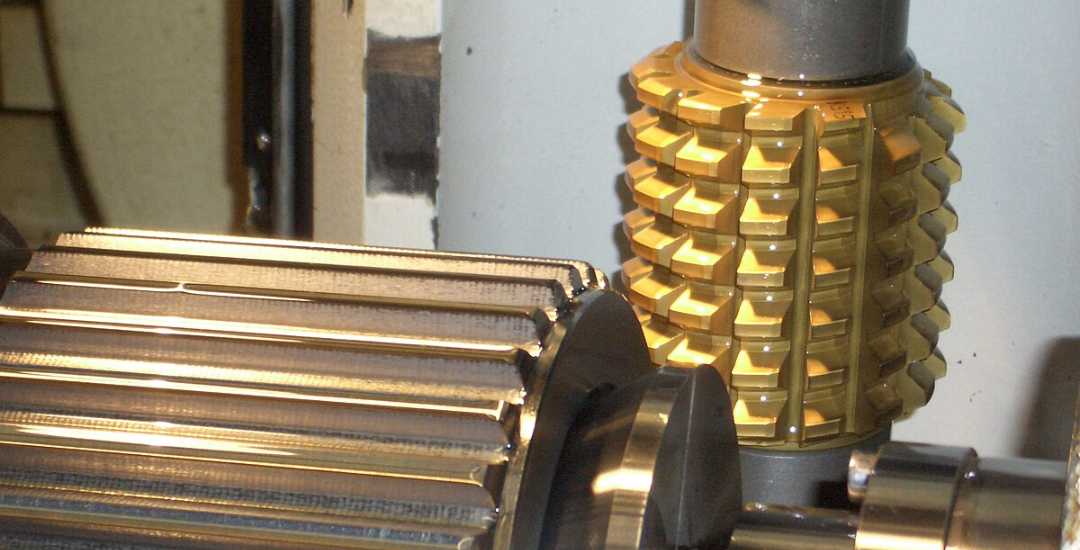
When the same gear profile must be produced repeatedly, hobbing is usually more efficient than öğütme each tooth individually. The process runs continuously, making it well suited for high-volume production.
Gear hobbing uses a rotating cutting tool called a hob to cut gear teeth into a blank. The hob and the workpiece rotate together in synchronized motion, and the teeth are formed progressively as the hob moves across the blank. One pass completes the entire set of teeth.
This continuous cutting action gives gear hobbing much higher productivity than milling, where each tooth is machined separately. Today, it is the standard process for high-volume production of external gears.
2. How Does Gear Hobbing Work?
Gear hobbing relies on precise synchronization between the hob and the gear blank. As both rotate together at a fixed ratio, the hob progressively generates the gear teeth while moving across the workpiece.
Synchronized Rotation
The hob and the gear blank are mounted on separate spindles. The two spindles are connected through a gear train or servo system that ensures they rotate at the correct ratio. For each revolution of the hob, the blank advances by one tooth pitch, creating the correct tooth spacing.
Hob Tilt Angle
The hob is tilted to match the lead angle of its threads. For spur gears, only a small tilt angle is required. For helical gears, the hob is tilted to match the helix angle of the gear being cut.
Feed Motion
The hob feeds into the gear blank until the full tooth depth is reached and then moves axially across the face width to generate the complete gear. Axial feed is the most common method for spur and helical gears. Radial feed is mainly used for worm gears and certain special applications, where the hob feeds directly toward the center of the blank.
Machine Types
Most gear hobbing is performed on vertical machines, where the hob is positioned above the workpiece. Horizontal machines are commonly used for shaft-type or long workpieces. Modern CNC hobbing machines support automated production, complex gear machining, and electronic synchronization, while conventional mechanical machines remain suitable for simple, high-volume jobs. High-speed machines are also available for small, fine-module gears.
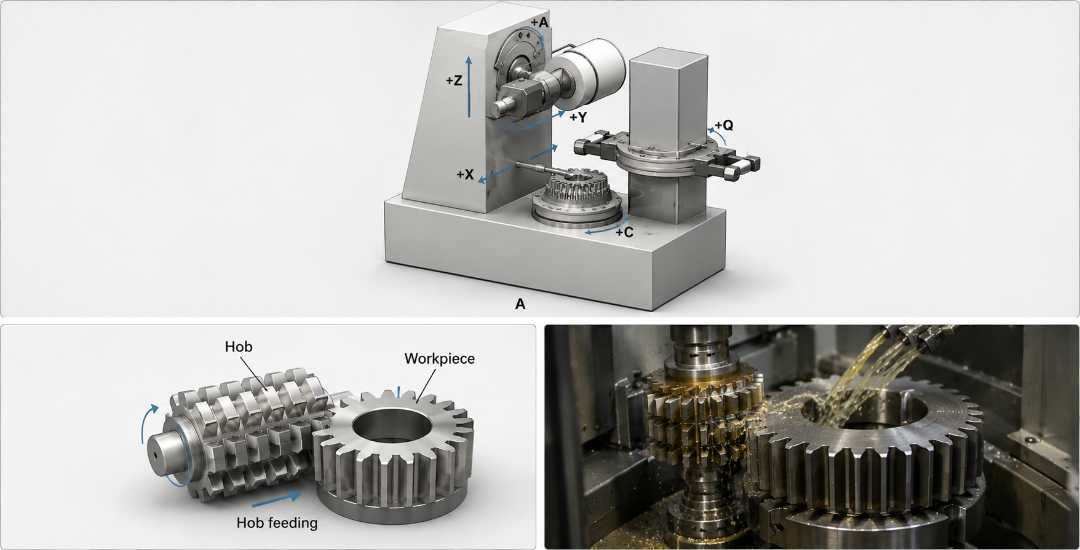
Accurate gear hobbing depends on proper synchronization, hob positioning, feed motion, and machine rigidity. These factors work together to produce consistent tooth spacing and tooth geometry throughout the cutting process.
3. Advantages of Gear Hobbing
Gear hobbing is the most widely used gear cutting method for volume production. It combines high productivity, consistent accuracy, and manufacturing flexibility, making it the preferred choice for many external gear applications.
High Efficiency
Hobbing is a continuous cutting process. The hob keeps cutting while the gear blank rotates, and all teeth are generated in one pass without stopping to index each tooth. Compared with milling, shaping, or broaching, hobbing offers much shorter cycle times, especially in high-volume production.
Good Accuracy
Typical production hobbing achieves approximately DIN 8 to DIN 10 accuracy, depending on machine condition, hob quality, workpiece material, and inspection method. This is sufficient for many industrial applications without additional finishing operations. The synchronized motion between the hob and the gear blank also produces consistent tooth spacing and profile.
Esneklik
A single hob can cut gears with different numbers of teeth as long as the module remains the same. By stocking hobs for different modules, manufacturers can produce a wide range of gears without requiring dedicated tooling for every tooth count.
Wide Material Range
Gear hobbing is suitable for a wide range of materials, including steel, cast iron, brass, bronze, aluminum, and some engineering plastics. Most gears are hobbed before heat treatment, while hardened gears typically require finishing operations such as gear grinding.
Otomasyon
Modern CNC hobbing machines support automatic loading and unloading, tool monitoring, in-process gauging, and unattended production. These features improve productivity, reduce labor requirements, and maintain consistent machining quality.
4. Disadvantages and Limitations of Gear Hobbing
Gear hobbing is highly efficient, but it also has clear limitations. Internal gears, certain gear geometries, and high-precision applications often require other manufacturing methods. Tooling cost and machine setup can also make hobbing less suitable for low-volume production.
Limited Gear Types
Hobbing works well for spur gears, helical gears, and worm gears. It cannot cut internal gears because the hob must approach the outside of the gear blank. It is also unsuitable for bevel gears, herringbone gears, and other non-cylindrical gear forms, which require specialized processes such as gear shaping or bevel gear cutting.
Accuracy Ceiling
Gear hobbing typically achieves DIN 8 to DIN 10 accuracy under normal production conditions. Applications requiring DIN 5 or better, such as automotive transmission gears or aerospace components, usually require gear grinding or other finishing operations after hobbing.
High Tooling Cost
High-quality or custom hobs represent a significant tooling investment, especially for small production runs. When only a few gears are required, setup time and tooling cost can make hobbing less economical than milling or shaping.
Skilled Operation Required
Successful gear hobbing depends on accurate machine setup and proper process control. Hob alignment, cutting speed, feed rate, tool condition, and machine maintenance all influence the final gear quality.
5. Gear Hobbing vs. Other Gear Manufacturing Methods

Several manufacturing methods are available for cutting gears, each offering different levels of productivity, accuracy, and application flexibility. The most suitable process depends on the gear type, production volume, and quality requirements.
Bakış açısı | Hobbing | Shaping | Frezeleme | Bileme |
|---|---|---|---|---|
Process principle | Continuous cutting (generation) | Reciprocating cutting (generation) | Form milling | Abrasive finishing |
Gear types | External spur, helical, worm | External, internal, double‑helical | External, special forms | All types (finishing) |
Yeterlik | Highest (high volume) | Ilıman | Düşük | Low (finishing) |
Typical accuracy | DIN 8–10 | DIN 7–9 | DIN 9–11 | DIN 3–5 |
Typical use | High‑volume gear production | Internal gears, double‑helical | Prototypes, repairs, small batches | Precision finishing after hobbing or shaping |
Hobbing is the most efficient process for producing external spur and helical gears in large quantities. Shaping is preferred for internal gears, while milling is better suited to prototypes, repairs, and special gear forms. Grinding is primarily used as a finishing process when higher accuracy or improved surface quality is required.
The best manufacturing method depends on gear geometry, production volume, and required accuracy.
Sources: DIN 3960–3967 gear tolerance standards; Machinery’s Handbook; AGMA gear manufacturing references; manufacturer technical data. Actual accuracy depends on machine condition, tooling, workpiece material, and inspection method.
6. Common Hobbing Problems and Troubleshooting
Even the best hobbing setup can run into trouble. Tools wear, machines drift, and materials vary. When problems appear, they usually show up on the tooth surface first, such as roughness, chatter, or profile errors. Catching the root cause quickly helps avoid scrap and downtime.
The table below summarizes several common hobbing problems, their likely causes, and recommended checks.
Sorun | Olası Nedenler | What to Check |
|---|---|---|
Rough tooth surface | Worn hob, incorrect cutting speed, poor chip evacuation, inadequate coolant | Check hob condition and replace if needed. Adjust cutting speed and coolant flow. |
Tooth profile error | Incorrect hob tilt angle, worn tool, machine misalignment | Verify hob angle setting and machine alignment. Re-sharpen or replace the hob. |
Tooth thickness deviation | Wrong hob position, incorrect depth of cut, indexing error | Check hob radial position and depth setting. Verify indexing mechanism. |
Chatter marks on teeth | Machine vibration, unbalanced hob, feed too high | Check machine stability. Balance the hob. Reduce feed rate. |
Rapid hob wear | Cutting speed too high, insufficient coolant, improper tool material | Reduce cutting speed. Increase coolant flow. Check if the hob material is correct for the workpiece. |
Most of these issues can be prevented through regular machine inspection, proper tool maintenance, and stable cutting conditions. Worn hobs, incorrect setup, and inadequate coolant management are among the most common causes of poor gear quality. Identifying problems early helps reduce scrap, extend tool life, and maintain consistent production quality.
7. Selection Guide: When to Choose Gear Hobbing
Gear hobbing is the preferred manufacturing method for high-volume external gears used in automotive, industrial machinery, power tools, agricultural equipment, and many other applications. However, the best manufacturing process depends on the gear geometry, production volume, and required accuracy.
The following guidelines can help determine whether gear hobbing is the right choice for a specific application.
Faktör | Choose Hobbing | Consider Other Methods |
|---|---|---|
Gear type | External spur, helical, or worm | Internal, bevel, herringbone, or non‑cylindrical |
Production volume | High volume (hundreds or thousands) | Low volume, prototypes, or one‑offs |
Required accuracy | DIN 8–10 | DIN 5 or better |
Gear size | Wide range | Very large or very small may need special machines |
Budget | Tooling and equipment costs can be amortized over volume | Limited tooling budget or low volume |
Hobbing is generally the best choice for external spur, helical, and worm gears produced in medium to high volumes where DIN 8 to DIN 10 accuracy is sufficient. Internal gears, very high precision requirements, and low-volume production are usually better served by shaping, milling, or grinding.
Sources: Industry standard DIN 3960-3967; machinery handbook. Actual values may vary depending on equipment, tooling, process parameters, and inspection method.
Çözüm
Gear hobbing remains one of the most efficient and widely used methods for producing external gears in large quantities. It offers an excellent balance of productivity, accuracy, and manufacturing cost for many industrial applications. Like every gear manufacturing process, its suitability depends on the gear design, production volume, and performance requirements.
At Beska, we manufacture precision gear-related components such as shafts, housings, flanges, and other custom CNC machined parts used in gear assemblies. We also help customers review drawings, materials, tolerances, and manufacturing requirements before production to support successful gear system projects.
 Turkish
 English
 Hebrew
 French
 Russian
 German
 Spanish
 Portuguese