


Bronze is a versatile material, widely used in industries ranging from engineering to art, for its strength, resistance to corrosion, and excellent conductivity. However, cutting this alloy presents unique challenges that require specialized techniques and precision.
Whether it’s shaping parts for heavy machinery or crafting intricate components for electronics, the bronze cutting process sets the stage for achieving the high tolerances and smooth finishes that these applications demand.
Despite its popularity, working with bronze requires the right tools and demands an understanding of the material’s behavior under cutting conditions. In this article, you’ll know the various bronze cutting methods, challenges, and best practices that ensure optimal results when working with this material.
1. Common Types of Bronze
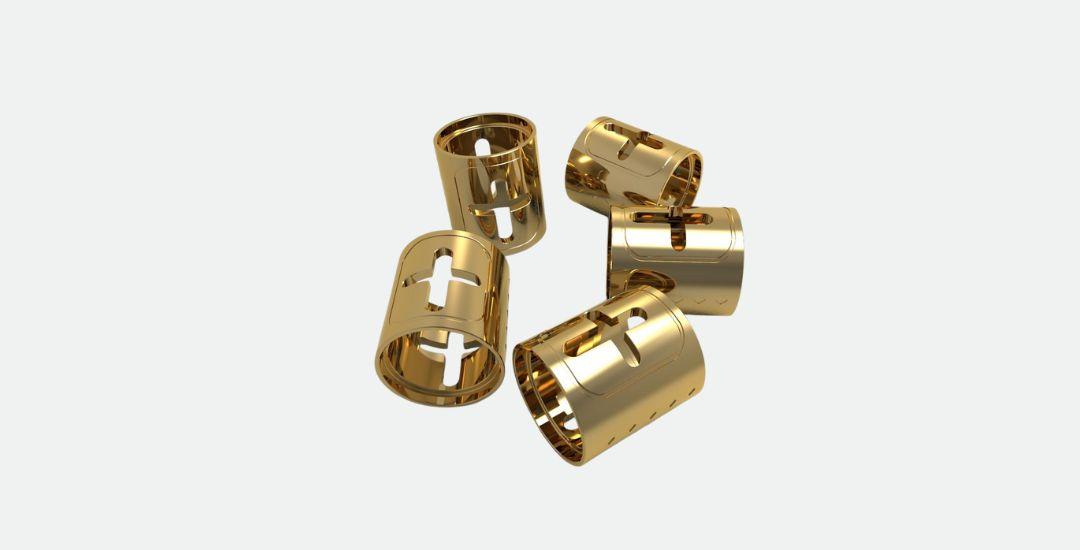
Bronze is an alloy primarily composed of copper, mixed with other elements such as tin, aluminum, silicon, and manganese. Each type of bronze has unique characteristics that affect its suitability for different applications. Here are the main types:
- Tin Bronze (Cu-Sn): Known for its good wear resistance and corrosion resistance, tin bronze is often used in precision parts like connectors. While it’s easy to machine, its high thermal conductivity can cause distortion in thin-walled components due to heat buildup during cutting.
- Aluminum Bronze (Cu-Al): With high strength and corrosion resistance, aluminum bronze is harder than many other alloys and can be challenging to cut. Its tendency to produce long, continuous chips can also lead to tool clogging if not properly managed.
- Silicon Bronze (Cu-Si): This alloy offers a balance of strength and conductivity, but its slightly uneven strength distribution can cause issues with drilling precision, especially when cutting small parts.
- Phosphor Bronze (Cu-Sn-P): Known for its excellent elasticity, phosphor bronze can become brittle if it contains too much phosphorus. Careful handling is needed during cutting to avoid cracking or chipping.
Before starting your project, it’s essential to choose the right material based on the desired mechanical properties and cutting requirements.
2. 6 Types of Cutting Bronze Methods
Cutting bronze effectively requires choosing the right method based on the part’s shape, size, and precision requirements. Here are six common cutting techniques:
CNC Tornalama (Lathe Cutting)

This method is ideal for cylindrical parts, such as shafts and bearings. Since bronze has a relatively low Brinell hardness (around 50–100 HB), it’s easier to cut and causes less tool wear during turning.
We typically use HSS or carbide tools—carbide grades like YG are especially effective for non-ferrous metals. With the right setup, it’s possible to achieve surface finishes suitable for sealing surfaces and tolerances in the IT7–IT8 range.
The advantages of choosing CNC turning for bronze cutting:
- Great for cutting outer diameters, internal bores, and faces
- High cutting efficiency and lower cost
- Suitable for batch production of rotating components
CNC Frezeleme (End Milling)
For bronze parts with flat, curved, or irregular surfaces, CNC milling is often the better choice. Whether vertical or horizontal milling is used, carbide end mills are preferred over HSS tools, which may wear too quickly at high speeds.
Bronze’s ductility can lead to burrs or built-up edges. To prevent this, we carefully manage feed rates and cutting speeds during milling. This ensures smoother finishes and protects the tool’s cutting edge.
Typical applications:
- Brackets, gears, and mounting plates
- Non-rotational, shaped bronze parts
Saw Cutting
Saw cutting is a fast way to divide large bronze bars or plates before further machining. It’s often used to prepare rough blanks for turning or milling.
We typically apply:
- Circular saws with HSS blades for thin or small materials
- Band saws with alloy-coated blades for thicker sections
Cutting fluid is essential here to avoid overheating, which can lead to warping or tool degradation.
Bileme

When tight tolerances or high surface quality is required, grinding is the finishing step. It’s used to fine-tune dimensions or remove burrs from bronze parts.
We rely on white aluminum oxide (corundum) wheels, which minimize unwanted chemical interaction with bronze. Depending on the requirement, we perform surface grinding or OD/ID grinding to achieve roughness values below Ra 0.8 μm.
Best for:
- Final finishing on tight-tolerance parts
- Flat or cylindrical bronze surfaces
Water Jet Cutting
For thicker bronze sheets or parts sensitive to heat, abrasive water jet cutting offers excellent results. It cuts by focusing a high-pressure stream of water mixed with abrasives like garnet, without introducing heat into the material.
This method creates clean edges without burrs and leaves no heat-affected zone. It’s especially useful when cutting expensive bronze grades like tin bronze, or for designs requiring complex internal contours.
Avantajları:
- Cuts through thick plates (even 10+ mm)
- No thermal distortion or discoloration
- Suitable for intricate shapes and large pieces
Lazer Kesim

Laser cutting is perfect for thin bronze sheets (≤5 mm) and decorative or electronic components. It uses a high-energy beam to melt and vaporize material, following precise digital paths from CAD files.
Key benefits:
- Fast processing speed (up to 10 m/min)
- Minimal heat-affected zone (≤0.1 mm)
- Smooth cuts (surface finish up to Ra 1.6 μm)
- Excellent for small-batch or prototype parts with intricate shapes
Sınırlamalar: Less accurate on thick plates; tolerances typically range from ±0.01 to ±0.05 mm.
Slow Wire Cutting
Wire EDM is a cold, stress-free process that uses a brass or zinc-coated wire to erode material through high-frequency electrical pulses. It’s especially suitable for cutting fine features, sharp corners, and tight tolerance parts.
Avantajları:
- Tolerances up to ±0.001 mm
- Perfect for cutting beryllium bronze or hardened alloys
- No mechanical force = no deformation
- Cuts extremely fine details (e.g., <0.1 mm gaps)
Trade-off: Slower and more expensive, best for high-precision, small-batch production.
3. When Not to Use CNC Machining for Bronze
CNC machining is widely used for bronze due to its precision and versatility, but it is not always the best choice. Several specific conditions can reduce efficiency, increase costs, or risk part quality:
Very Thin Bronze Sheets
Thin bronze can deform easily under cutting forces, leading to warping or inaccurate dimensions. In these cases, waterjet or laser cutting can reduce mechanical stress and maintain flatness.
Simple or Rough-Cut Parts
For components with uncomplicated shapes or loose tolerances, the setup time, tool wear, and cost of CNC machining may outweigh its benefits. Simpler methods like sawing or stamping can be more efficient.
High-Volume Repetitive Parts
When producing large batches of small bronze components, CNC machining may be slower and less cost-effective compared with automated forming or stamping. Tool wear and frequent adjustments can add hidden costs.
Parts Sensitive to Thermal or Mechanical Stress
Some bronze alloys, especially aluminum or silicon-rich variants, are prone to distortion or surface defects under high cutting forces. Alternative processes may better preserve material properties and surface integrity.
CNC machining should be chosen after evaluating part thickness, complexity, production volume, and alloy characteristics to ensure that precision, cost, and efficiency are properly balanced.
4. Cutting Techniques Not Recommended for Bronze
Except for these ideal methods, there are certain cutting methods that aren’t suitable for bronze.
Oxy-Acetylene Cutting: Bronze’s high thermal conductivity makes it difficult to form a localized molten pool, leading to oxidation, deformation, and even cracking.
Plasma Cutting: While effective for other metals, plasma cutting causes significant heat-affected zones, which can degrade the material’s mechanical properties, making it unsuitable for precision work.
Gas Cutting: Similar to oxy-acetylene, gas cutting fails due to bronze’s inability to burn, resulting in poor cutting quality.
High-Speed Grinding (Without Cooling): Without proper cooling, bronze can overheat, causing oxidation and potential cracking, especially for precision components.
5. Common Mistakes in Cutting Bronze
Cutting bronze can be straightforward in principle, but several recurring mistakes often compromise efficiency, surface quality, or dimensional accuracy. Being aware of these pitfalls allows engineers and machinists to plan operations more effectively:
Using Inappropriate Cutting Parameters
Applying feed rates or spindle speeds that do not match the alloy hardness can cause excessive tool wear or poor surface finish. Harder alloys require slower cutting speeds, while softer grades may allow faster feeds without compromising quality.
Neglecting Chip Evacuation
Improper chip removal can lead to material accumulation in the cut zone, scratching the surface or jamming the tool. For deep pockets or narrow slots, continuous clearing or compressed air/lubricant use is critical.
Overlooking Thermal Effects
Although bronze conducts heat well, localized hot spots can form during cutting, affecting surface finish and dimensional stability. Using appropriate coolant or lubricant and avoiding prolonged engagement in one area can minimize these issues.
Underestimating Burr Formation
Edges, holes, and corners in bronze often develop burrs due to the alloy’s plasticity. Ignoring burr management can increase post-processing time and cause assembly fit issues.
Insufficient Post-Processing Planning
Failing to plan for deburring, polishing, or finishing after cutting can lead to additional costs and delays. Anticipating finishing needs allows selection of cutting parameters that minimize burrs and surface defects.
Careful selection of cutting parameters, tooling, and cooling strategies, along with attention to burr control and post-processing, is essential to achieve consistent, high-quality results in bronze cutting.
6. Challenges in Cutting Bronze
Cutting bronze involves several key challenges that require careful attention to ensure high-quality results. Here are the main issues and how they affect the process:
1. Chip Control
One of the most frequent challenges in bronze cutting—especially with aluminum bronze—is the formation of long, ribbon-like chips. These chips tend to wrap around the tool or part, making it difficult to maintain cutting visibility and cooling. Worse yet, the high ductility of bronze often leads to built-up edge (BUE), where chips adhere to the cutting edge. This can degrade tool performance, increase friction, and result in poor surface finish.
For instance, when machining a structural bronze bracket, excessive chip wrapping can cause tool overheating, reduce tool life, or even damage the part’s surface. Using proper chip breakers, high-pressure coolant, and adjusting cutting parameters are key strategies to minimize this issue.
2. Surface Finish
Although bronze is considered a relatively “easy-to-cut” material, achieving a consistent surface finish requires attention. Alloys like tin bronze are easier to machine but still prone to visible tool marks or micro-grooves—especially when the cutting tool is dull or parameters are misconfigured.
For high-precision components such as electrical contacts or decorative pieces, surface irregularities can not only affect appearance but also compromise functionality. Regular tool inspection, correct feed rates, and using sharp carbide tools can significantly improve surface quality.
3. Thin Wall Distortion
Due to bronze’s high thermal conductivity, thin sections tend to warp during machining, particularly under localized heat. When working with bronze sheets or flanges as thin as 0.3–0.5 mm, even light cutting forces can cause bending or vibration.
For example, laser cutting or turning a thin-walled bronze sleeve without adequate cooling can result in dimensional deviation. To avoid this, air cooling or coolant misting should be used, along with reduced depth-of-cut and multi-pass strategies.
4. Workholding for Irregular Shapes
Complex bronze components—such as parts with angled holes, curved profiles, or asymmetrical features—can be difficult to fixture using standard clamps. Poor workholding increases the risk of vibration, tool deflection, or misalignment, especially when precision is critical.
In such cases, custom jigs or soft jaw fixtures are often required to hold the workpiece securely without deforming the bronze. This is particularly true for decorative or structural components in art installations, automotive trim, or aerospace brackets.
7. Quality Control in Bronze Cutting
To ensure consistent, high-quality cuts in bronze involves managing several key factors:
Tool Selection:
Selecting the proper cutting tool is the first line of defense against poor quality. For most bronze alloys—including tin bronze and aluminum bronze—carbide tools are recommended due to their high hardness and wear resistance. High-speed steel (HSS) tools may be acceptable for softer bronze grades, but they tend to dull more quickly when cutting harder alloys like aluminum bronze (which can reach Brinell hardness ~170HB).
Also important is the tool geometry: positive rake angles and sharp edges help reduce friction and minimize the tendency for chip adhesion (built-up edge), which improves both tool life and surface quality.
Cutting Parameters:
Proper feed rate and cutting speed are crucial. Adjusting these parameters can minimize heat buildup, prevent tool wear, and ensure a clean cut.
Here’s a general reference table for typical parameters when roughing and finishing common bronze alloys:
| Parametre | Roughing (e.g., C95400) | Finishing (e.g., C93200) |
| Kesme Hızı | 80–150 m/min | 150–300 m/min |
| Feed Rate | 0.1–0.3 mm/rev | 0.05–0.15 mm/rev |
| Kesme derinliği | 1–3 mm | 0.2–0.5 mm |
Post-Cutting & Inspection Processes:
After cutting, the parts require post-machining treatment to meet visual and dimensional standards. Common post-processing steps include:
- Deburring: Essential for removing sharp edges and micro-burrs, especially after saw cutting or milling.
- Polishing: For aesthetic or functional reasons (e.g., reducing friction in sliding components), polishing may be needed to bring the surface roughness down to Ra 0.8μm or better.
- Dimensional inspection: Using calipers, micrometers, or CMM machines to ensure tolerances are within spec (typically IT7–IT9 for bronze parts).
8. The Applications of Bronze Cutting

Bronze cutting is essential in creating precise components for various industries:
Mechanical Parts
Parts like bearings, bushings, and gears are cut from bronze for use in heavy machinery and automotive applications. These components benefit from bronze’s wear resistance and ability to withstand high pressure.
Elektronik
In electronics, bronze is cut to make connectors and terminals. Its excellent conductivity and corrosion resistance make it ideal for electrical components that need to maintain stable connections over time.
Art and Decorative Pieces
Bronze is often cut for sculptures, medals, and other decorative items. Its ability to take on intricate details and develop a unique patina makes it a favorite for artists and designers.
9. Real-world Cases of Bronze Cutting
Our years of experience with bronze cutting have helped us refine our processes and deliver high-quality components for various industries. Here are some examples:
High-Precision Bronze Bearings

For a European client from a startup, we used CNC turning to produce wear-resistant bronze bearings with a surface roughness of Ra 0.8 μm and a tolerance of ±0.01 mm. These bearings were critical for machinery that required both high performance and long-term durability, and our precision CNC turning ensured they met stringent operational standards.
Electronic Connectors for 5G Equipment
In late 2024, we utilized high-speed stamping to produce precise bronze connectors for 5G communication devices. These connectors needed to meet strict dimensional and conductivity standards to ensure optimal signal transmission. Our careful control over the stamping process guaranteed both dimensional accuracy and consistent conductivity, key factors for high-performance electronics.
Marine Components
For a shipbuilding project, we employed five-axis milling to produce aluminum bronze valve bodies. These parts were subject to a rigorous 1000-hour salt spray test to ensure corrosion resistance. With our specialized treatments and precise machining, the valve bodies passed the test, making them suitable for long-term use in harsh marine environments.
Çözüm
Bronze cutting is a specialized process that requires expertise in understanding material properties, choosing the right cutting techniques, and applying strict quality control. By selecting the appropriate tools and optimizing cutting parameters, manufacturers can produce bronze components that meet the highest industry standards.
When looking for a supplier, whether for mechanical parts or decorative designs, contacting a team like the Beska team, who understands the intricacies of bronze cutting, can ensure the best possible outcome.
Deeper into Our Resources
İçgörü dolu okumalar için, sizin için özel olarak önerilen makalelerden oluşan bir liste hazırladık:
- How to Polish Bronze
- Bronze vs Brass
- CNC Machining Bronze
- Yüzey İşlemleri
- How to weld Stainless Steel
- Sheet Metal Forming Service
 Turkish
 English
 Hebrew
 French
 Russian
 German
 Spanish
 Portuguese