


A steel gear or shaft often needs two very different properties at the same time: a hard surface to resist wear and a tough core to handle repeated loads. Carburizing is one way to achieve this combination by introducing additional carbon into the surface of suitable steel before hardening.
The process is widely used for gears, shafts, bearings, pins, and other components exposed to wear and contact stress. Its effectiveness depends on more than surface hardness alone. Steel grade, case depth, heat treatment, and dimensional change after quenching all influence the final performance of a carburized part.
1. What Is Carburizing?
Carburizing is a thermochemical case-hardening process in which steel is heated in a carbon-rich environment, allowing carbon to diffuse into its surface. It is commonly applied to low-carbon and low-alloy steels at temperatures where the steel is austenitic, often within the range of approximately 850°C to 950°C.
As carbon diffuses inward, a carbon concentration gradient develops from the surface toward the core. After carburizing, the component is typically quenched and tempered. The carbon-enriched surface can then develop a hard martensitic case, while the lower-carbon core retains greater toughness.
The result is a component with high surface hardness and wear resistance combined with a tougher supporting core. Case depth, surface carbon content, steel grade, and the subsequent hardening cycle all influence the final properties.
2. How the Carburizing Process Works
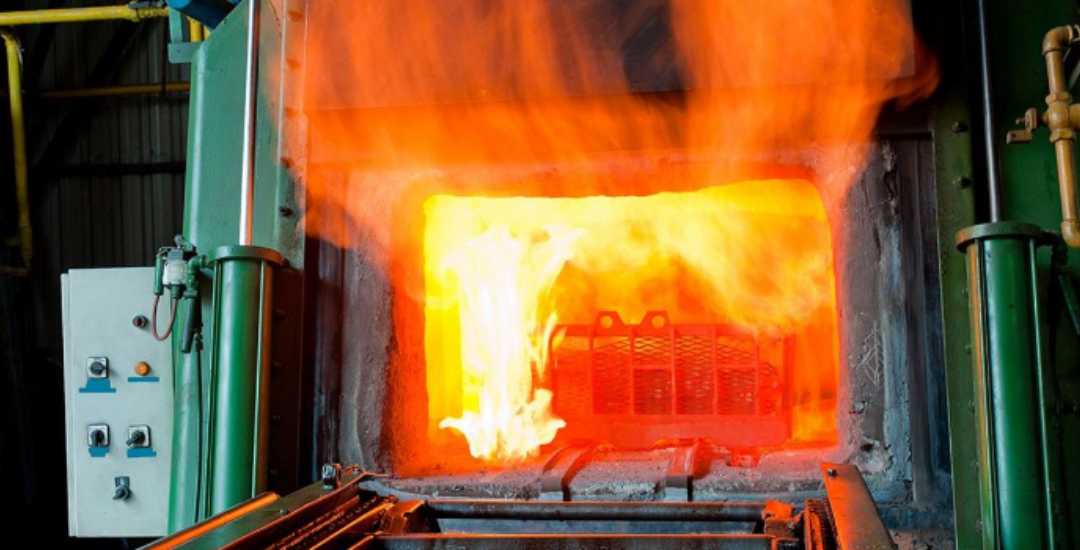
A typical gas carburizing cycle includes several stages that control carbon diffusion and develop the final hardened case. The exact sequence and parameters vary with the steel grade, required case depth, furnace, and hardening method.
1. Preparation
Parts are cleaned to remove oil, scale, and other contaminants that could interfere with surface treatment.
2. Heating
The components are heated to the required carburizing temperature, where the steel develops an austenitic structure capable of absorbing carbon.
3. Carburizing
A carbon-rich furnace atmosphere supplies carbon to the steel surface. Temperature, time, and carbon potential are controlled according to the required surface carbon level and case depth.
4. Diffusion
The atmosphere may then be adjusted to allow carbon to diffuse farther below the surface and develop the required carbon profile through the case.
5. Quenching
After carburizing, the component is hardened by controlled cooling. The carbon-enriched case transforms into a hard microstructure, typically dominated by martensite.
6. Tempering
Tempering is commonly performed after quenching to reduce stresses and adjust the final hardness and mechanical properties.
The required case depth and carbon profile develop through the combined control of temperature, carbon potential, and time, while the subsequent quenching and tempering steps determine much of the final hardness and dimensional response.
3. Key Carburizing Methods
Different carburizing methods use different ways to introduce carbon into the steel surface. The appropriate process depends on factors such as case-depth requirements, part geometry, production volume, and process-control needs.
Gas Carburizing
Gas carburizing uses a controlled furnace atmosphere containing carbon-bearing gases to introduce carbon into the steel surface. It is widely used for batch and production heat treatment because the carbon potential and process conditions can be controlled throughout the cycle.
Careful atmosphere control is important to maintain consistent carburizing conditions and reduce problems such as excessive carbon buildup or soot formation.
Vacuum Carburizing
Vacuum carburizing, also known as low-pressure carburizing, introduces carbon-bearing gases under low-pressure conditions. It provides a clean processing environment and precise control over carbon delivery.
The process requires specialized equipment and is often considered for precision components where surface cleanliness and controlled processing are important.
Pack Carburizing
Pack carburizing places steel components in a sealed container surrounded by carbon-rich solid material. During heating, carbon-containing gases form inside the container and supply carbon to the steel surface.
Compared with modern controlled-atmosphere processes, pack carburizing offers less precise control over atmosphere and case development, so it is less common for high-volume precision production.
Liquid Carburizing
Liquid carburizing treats components in a molten salt bath containing carbon-bearing compounds. The liquid medium provides rapid heat transfer and close contact with the component surface.
Some traditional salt-bath processes require strict handling, environmental, and safety controls, which can limit their use in modern production environments.
Plasma Carburizing
Plasma carburizing uses ionized gas to assist carbon transfer into the steel surface. It provides controlled treatment conditions and can be useful where more specialized surface processing is required.
Its main limitation is the need for dedicated equipment and more specialized process control compared with conventional furnace carburizing.
4. Carburizing Steel Grades: What Materials Are Used?
Carburizing is commonly applied to low-carbon and low-alloy steels that can develop a hard surface case while retaining suitable core properties after heat treatment. Material selection depends on required case depth, core strength, hardenability, part size, and service conditions.
AISI 8620
AISI 8620 is a widely used carburizing alloy steel containing nickel, chromium, and molybdenum. Its combination of hardenability and core toughness makes it suitable for gears, shafts, pins, and other components exposed to wear and repeated loading.
AISI 1018
AISI 1018 is a low-carbon steel that can be carburized when high surface hardness is required without demanding high core hardenability. Its lower alloy content makes it suitable for relatively simple components, but its lower hardenability can limit core strength in larger sections compared with alloy carburizing steels.
16MnCr5 and 20MnCr5
16MnCr5 and 20MnCr5 are commonly used European carburizing steel grades. They provide a useful combination of case hardenability and core strength and are frequently specified for gears, shafts, and transmission components.
18CrNiMo7-6
18CrNiMo7-6 is a higher-alloy carburizing steel used for heavily loaded components requiring greater hardenability and core strength. Typical applications include heavy-duty gears and drivetrain components.
The appropriate carburizing steel should be selected according to the required case properties, core strength, section size, loading conditions, and subsequent heat-treatment process. A higher-alloy grade is not automatically better; the material should match the actual performance requirements of the part.
5. Benefits of Carburizing
Carburizing is particularly useful when a component needs high surface hardness and wear resistance while retaining a tougher supporting core.
Improved Wear Resistance
After carburizing and hardening, the carbon-enriched surface develops a hard case that resists wear under sliding and rolling contact. This makes the process well suited to gears, shafts, pins, and other components with heavily loaded contact surfaces.
Better Fatigue Performance
A properly carburized and hardened case can improve resistance to contact fatigue and repeated loading. This is particularly important for gears and drivetrain components exposed to cyclic stresses over long service periods.
Hard Surface with a Tougher Core
Unlike through-hardening, carburizing creates different properties across the component. The surface is hardened for wear resistance, while the lower-carbon core retains greater toughness and can better support impact and mechanical loads.
Suitable for Production Volumes
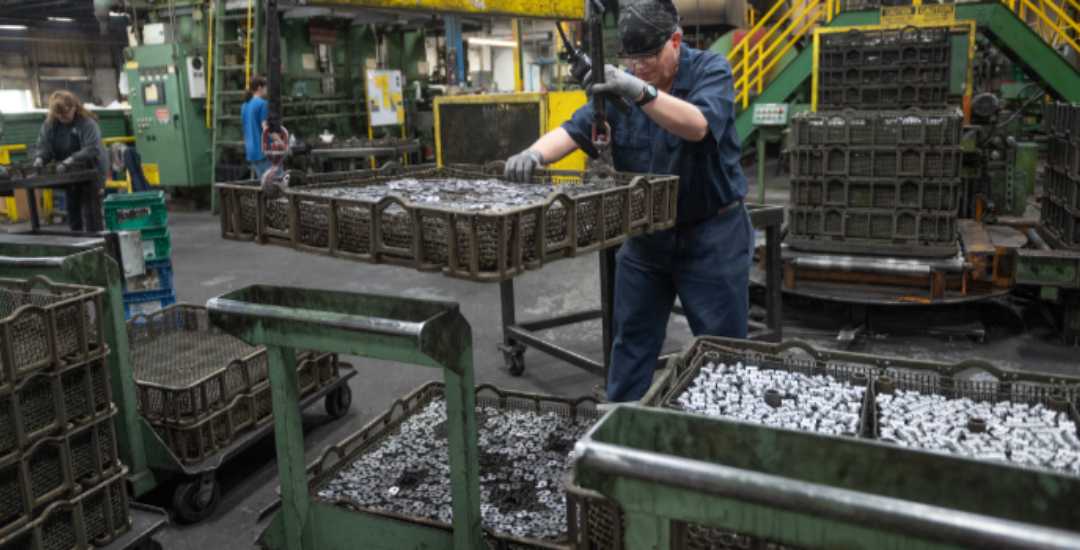
Gas carburizing allows multiple components to be processed in a furnace batch, making it practical for many medium- and high-volume production applications. Actual cost depends on the steel grade, case-depth requirement, part size, batch quantity, and subsequent finishing operations.
This balance of surface durability and core toughness is what makes carburizing valuable for demanding mechanical parts.
6. Limitations and Risks You Need to Know
Carburizing can significantly improve surface hardness and wear performance, but the process also introduces several factors that need to be considered during part design and production.
| Limitation | What to Consider |
| Distortion and Dimensional Change | Heating, phase transformation, residual stress, part geometry, fixturing, and quenching can all affect final dimensions. Precision components may require machining allowance for post-heat-treatment finishing. |
| Process Control | Case depth, carbon profile, and hardness depend on controlled temperature, time, atmosphere, and hardening conditions. Steel composition and furnace loading can also affect consistency. |
| Additional Finishing | Tight-tolerance or critical surfaces may require grinding or other finishing after heat treatment, adding production time and cost. |
| Selective Hardening | Areas that should remain unaffected may require copper plating or suitable stop-off coatings. For highly localized hardening, processes such as induction hardening may also be considered. |
| Surface Carbon Control | Excessive surface carbon can contribute to retained austenite, excessive carbide formation, or other undesirable microstructural conditions. |
| Corrosion Protection | Carburizing improves hardness and wear resistance but does not inherently improve corrosion resistance. Additional surface protection may be required in corrosive environments. |
These factors should be evaluated alongside the part’s tolerance, material, and service requirements before carburizing is specified.
7. Common Applications of Carburizing
Carburizing is widely used for steel components that combine repeated surface contact or wear with substantial mechanical loading. Typical applications include:
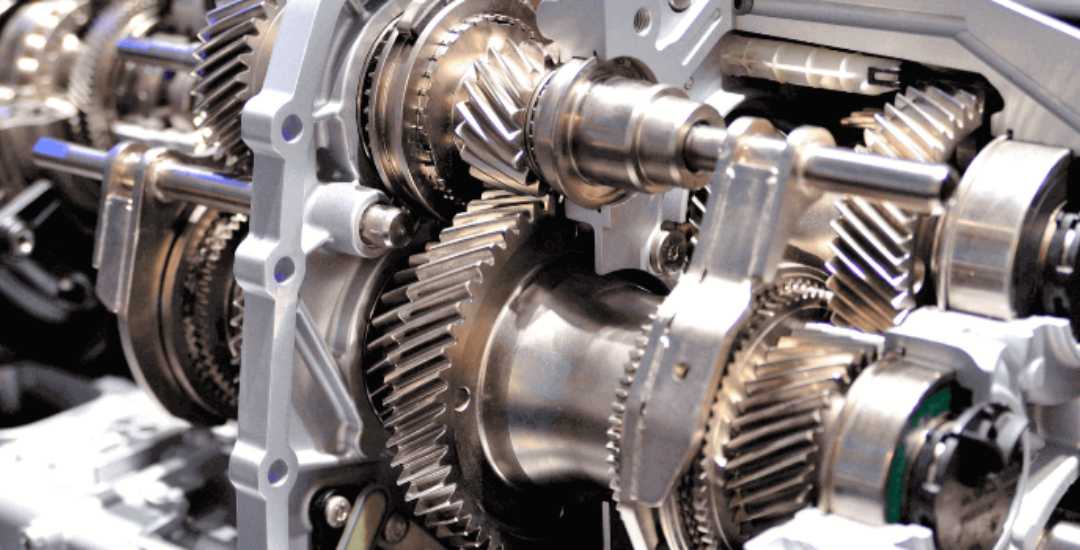
- Automotive Gears: Transmission, planetary, pinion, and differential gears benefit from a hard case that resists tooth-surface wear and contact fatigue while maintaining a tougher supporting core.
- Camshafts and Crankshafts: Selected shaft and journal applications can use case hardening to improve wear resistance at contact surfaces while retaining the strength and toughness required to carry cyclic loads.
- Bearings: Certain bearing races and rolling-contact components use carburized steels where high surface hardness, contact-fatigue resistance, and core support are required together.
- Heavy Machinery Components: Pins, bushings, gears, and drivetrain components exposed to abrasive wear and impact loading can benefit from the combination of a hardened case and tougher core.
These applications share the same basic requirement: the surface must resist wear and contact loading without making the entire component uniformly hard and brittle.
8. Carburizing vs Nitriding vs Induction Hardening
Carburizing, nitriding, and induction hardening can all improve surface performance, but they differ in material compatibility, case characteristics, heat input, and dimensional response.
| Feature | Carburizing | Nitriding | Induction Hardening |
| Typical Steel Types | Low-carbon and carburizing alloy steels | Alloy steels with suitable nitride-forming elements are commonly preferred | Medium- and high-carbon steels with sufficient hardenability |
| Process Temperature | Typically 850–950°C | Typically 500–580°C | Rapid localized heating above the transformation temperature |
| Typical Case Depth | Medium to deep | Generally shallow | Can range from shallow to relatively deep depending on process and geometry |
| Surface Hardness | High | Very high | High |
| Distortion Risk | Higher due to high-temperature treatment and quenching | Generally lower because rapid quenching is normally not required | Depends strongly on heating pattern, geometry, and quenching |
| Cycle Time | Moderate to long | Generally long | Short |
| Selective Hardening | Possible with masking | Possible with masking | Well suited to localized hardening |
| Typical Use | Gears, shafts, bearings, heavily loaded components | Precision wear parts, dies, molds, gears | Shafts, gears, bearing surfaces, and localized wear areas |
Actual case depth, hardness, and dimensional change depend on the steel grade, process parameters, geometry, and heat-treatment specification.
The best choice depends on the required case depth, base material, distortion tolerance, and whether the entire surface or only selected areas need hardening.
Conclusion
Carburizing combines a hard, wear-resistant case with a tougher supporting core, making it a widely used surface-hardening process for gears, shafts, bearings, and other heavily loaded steel components.
The final result depends on more than hardness alone. Steel grade, case depth, dimensional requirements, distortion risk, and post-heat-treatment finishing should all be considered before the process is specified. For parts with demanding tolerances or surface requirements, planning the machining and heat-treatment sequence early can reduce unnecessary rework later.
Need help with a carburized CNC machined part? Send us your drawing to review the material, tolerances, and post-heat-treatment machining requirements.
 English
 Hebrew
 Turkish
 French
 Russian
 German
 Spanish
 Portuguese