


A new injection-molded part does not always need a full production mold from the start.
When the design is still being validated, a prototype mold can provide real molded parts for fit, function, assembly, and material testing while leaving more room for design changes. Once the part and production requirements are stable, the tooling priorities shift toward durability, repeatability, and long-term output.
This article compares prototype molds and production molds in terms of design, cost, tool life, production requirements, and the role of bridge tooling between them.
1. What Is the Difference Between Prototype and Production Molds?
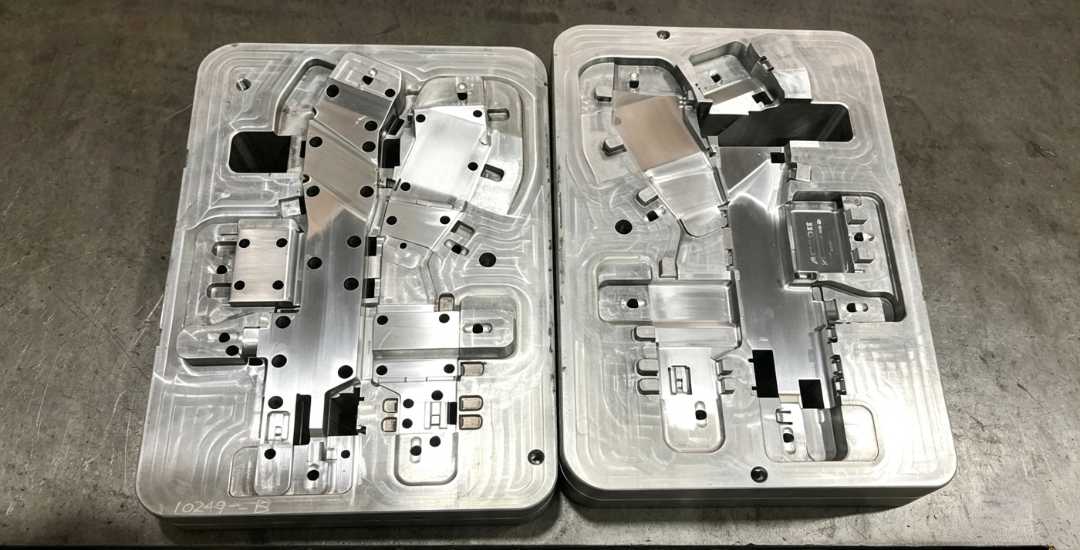
A prototype mold is built mainly to produce real molded parts for design validation. It allows engineers to check fit, function, assembly, material behavior, and molding performance before the product and production requirements are fully finalized.
A production mold has a different priority. It is designed to run repeatedly over a longer production life, with greater attention to cycle consistency, ejection, cooling, automation, maintenance, and dimensional stability.
The difference is therefore not defined by mold material alone. Aluminum, pre-hardened steel, or hardened steel may be selected depending on the required tool life, resin, part geometry, surface finish, and production plan. What matters most is what the mold is expected to prove or produce.
2. Prototype Mold vs Production Mold: Key Differences
Prototype and production molds may use similar molding principles, but they are designed around different priorities. The main differences appear in tooling investment, expected service life, production efficiency, and how much flexibility is needed during development.
| גוֹרֵם | Prototype Mold | Production Mold |
| מטרה ראשית | Design, material, and process validation | Repeatable long-term production |
| Tooling Investment | Usually lower because the tool is built around shorter-term requirements | Usually higher due to more robust tooling, cooling, automation, and durability requirements |
| זמן אספקה | Generally shorter, especially when the mold design is simple | Generally longer because more engineering, machining, fitting, and validation may be required |
| Mold Material | Often aluminum or pre-hardened steel | Often pre-hardened or hardened steel, depending on the application |
| Expected Tool Life | Designed for validation or limited production | Designed around the required long-term production life |
| Cavity Strategy | Often single-cavity or relatively simple | May use multi-cavity layouts to meet production output targets |
| Cooling and Automation | Can be simplified when cycle time is not the main priority | More strongly optimized for cycle consistency, ejection, and automated production |
| Design Changes | Generally easier to accommodate | Usually more involved once the tooling has been finalized |
| Best Fit | Evolving designs, testing, and early production | Stable designs with established production requirements |
These differences are guidelines rather than fixed definitions. A prototype mold can sometimes support production, while a production mold does not always need hardened steel or multiple cavities. The appropriate tooling depends on what the mold needs to achieve over its expected service life.
3. How Mold Design Changes from Prototype to Production
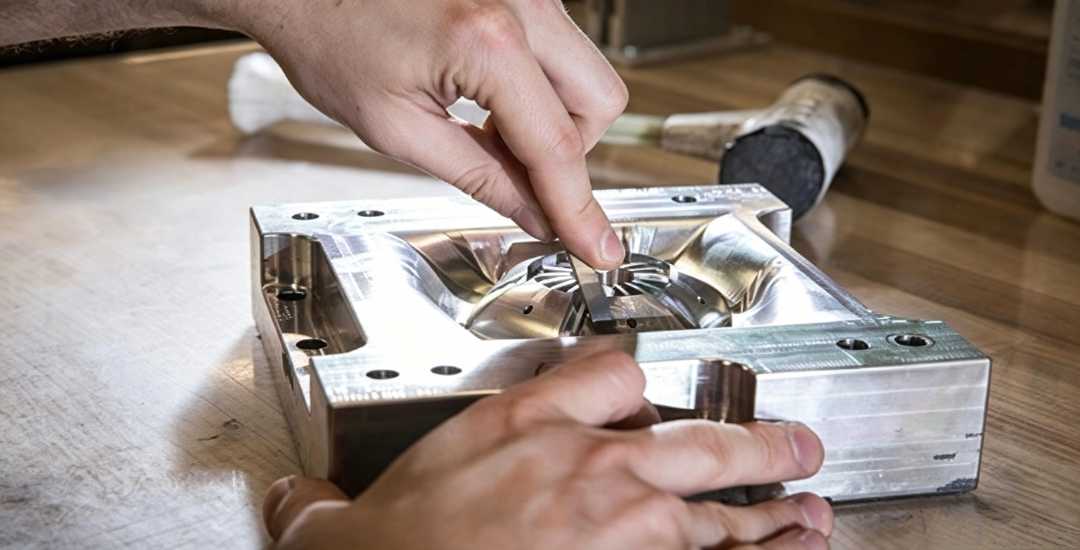
As tooling moves from prototype validation to long-term production, the mold design usually becomes more focused on repeatability, cycle consistency, maintenance, and output rather than simply producing acceptable parts.
Cooling
Prototype molds may use a simpler cooling layout when cycle time is not the main priority. Production molds require more controlled cooling because uneven mold temperature can affect cycle time, shrinkage, warpage, and dimensional consistency over long runs.
Ejection and Automation
A prototype run can tolerate more manual intervention during setup or part removal. In production, the ejection system needs to work reliably through repeated cycles with minimal operator involvement.
This may require more robust ejector layouts, automated part removal, or other features that support continuous production.
Slides and Lifters
Undercuts often require slides, lifters, or other moving mold components. These features add complexity to both prototype and production tooling, but production molds place greater emphasis on wear resistance, repeatable movement, and long-term maintenance.
Prototype tooling may sometimes use a simpler mechanism when production speed and automation are less important.
Cavity Count
Prototype molds are often kept relatively simple so design changes remain manageable. Once demand and part design are established, production tooling may use multiple cavities to increase output and reduce the tooling cost allocated to each part.
The appropriate cavity count still depends on part size, filling balance, press capacity, production demand, and mold complexity.
The main difference is therefore not that production molds use completely different molding principles. They are engineered to repeat the same molding cycle reliably over a much longer production period.
4. How Cost, Volume, and Tool Life Affect the Decision
A lower-cost mold is not always the lowest-cost option over the life of a product. Tooling decisions need to consider the initial mold investment together with expected production volume, tool life, maintenance, and the efficiency of each molding cycle.
Upfront Tooling Cost
Prototype molds usually require less initial investment because they are built around validation or limited production needs. Production molds may require more durable materials, more complex cooling, additional cavities, automation features, and longer validation before release.
That higher investment only makes sense when the expected production requirements justify it.
Expected Production Volume
Higher volume generally makes a more durable and efficient mold easier to justify, but there is no universal part quantity at which a project should automatically switch from prototype to production tooling.
A low-volume part using an abrasive resin or requiring demanding surface quality may justify more durable tooling early. In other cases, a well-designed aluminum tool may support a much longer production run than expected.
Tool Life and Production Conditions
Tool life depends on more than mold material. Resin abrasiveness, part geometry, cavity pressure, surface requirements, moving components, maintenance, and molding conditions all influence how long a tool can remain productive.
The useful question is therefore not simply how many parts the mold can make, but whether it can maintain the required part quality and production rate throughout the planned program.
For most projects, the tooling strategy should be evaluated against the expected lifetime demand rather than a fixed volume threshold. A higher initial mold investment can be justified when it improves long-term repeatability, output, and tool life, while a simpler tool may be more practical when the design or demand is still uncertain.
5. Where Bridge Tooling Fits
Not every project moves directly from prototype validation to full production tooling. Bridge tooling can fill the gap when the design is largely validated but long-term production requirements are still developing.
A bridge mold is typically built to support early production, market launch, or ramp-up while the final production tool is being completed or while demand is still being confirmed. It can also provide additional time to evaluate part quality, assembly performance, and production requirements before committing to a more complex long-life mold.
Compared with a prototype mold, bridge tooling is usually designed with more attention to production consistency and expected output. Compared with a full production mold, it may use simpler tooling architecture, fewer cavities, or a shorter intended service life.
Bridge tooling is especially useful when the project needs real production parts but still benefits from some flexibility. It gives engineering and procurement teams a way to move forward without treating early demand as a final long-term production forecast.
6. How to Choose the Right Tooling Strategy
The right tooling strategy depends on how stable the product and production plan already are. A project with an evolving design should not be evaluated in the same way as a mature part with established long-term demand.
Design Maturity
If dimensions, materials, assembly features, or cosmetic requirements are still changing, prototype tooling usually leaves more room for modification and validation.
Once the part design is stable and major changes are unlikely, investment in longer-life production tooling becomes easier to justify.
Expected Production Demand
Consider both the immediate requirement and the expected lifetime volume. Early demand may support prototype or bridge tooling, while sustained production may justify a mold designed around longer service life, higher output, and reduced manual intervention.
Volume should be treated as one decision factor rather than a fixed threshold.
Resin and Wear Conditions
The molded resin can strongly influence tooling requirements. Abrasive or heavily filled materials may increase wear on cavities, gates, slides, and other mold components, making more wear-resistant tooling appropriate even when the planned volume is not especially high.
Corrosive resins or demanding surface requirements can also influence mold material and steel selection.
Surface Finish and Dimensional Requirements
Parts with demanding cosmetic surfaces, optical features, tight dimensional control, or critical repeatability may require more attention to mold material, polishing, cooling, venting, and long-term tool stability.
A prototype tool may still be useful for validation, but the final production mold should reflect the actual quality requirements of the finished part.
Timeline and Market Risk
When parts are needed quickly or demand is still uncertain, prototype or bridge tooling can reduce the commitment made before the product or market is fully proven.
If the design, demand, and production plan are already established, building directly for production may avoid an additional tooling stage.
The best tooling strategy is therefore based on the complete project rather than one variable alone. Design maturity, expected demand, resin, quality requirements, and timeline should all be reviewed together before deciding whether prototype, bridge, or production tooling is the better fit.
מַסְקָנָה
Prototype molds and production molds are built for different stages of a product’s development. Prototype tooling gives teams more flexibility to validate the part and make changes, while production tooling is designed around repeatability, tool life, and long-term manufacturing.
The right choice depends on how mature the design is, how much production is expected, what resin and quality requirements are involved, and how quickly the project needs to move forward. In some cases, bridge tooling provides a practical step between validation and full production.
For custom injection molding projects, Beska can review part design, material, expected production demand, and tooling requirements to help determine whether prototype, bridge, or production tooling is the better fit.
 Hebrew
 English
 Turkish
 French
 Russian
 German
 Spanish
 Portuguese