


CNC machining fixtures locate and secure a workpiece so it can be machined from a consistent reference. Depending on the part, the workholding may be as simple as a vise and soft jaws or as specialized as a dedicated fixture with locating pins, supports, and custom clamps.
Fixture design affects much more than whether a part stays in place. Locating accuracy, clamping force, rigidity, tool access, and chip clearance can all influence repeatability, dimensional control, surface finish, and setup efficiency. The most suitable fixture therefore depends on the part geometry, machining operation, tolerance requirements, and production volume.
1. Why Fixture Design Matters in CNC Manufacturing
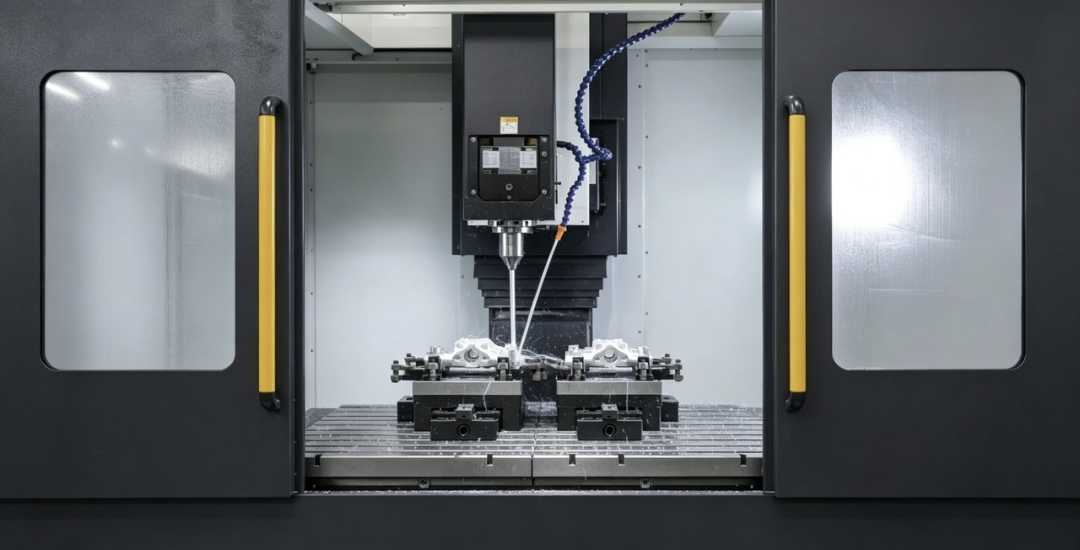
A fixture does more than hold a workpiece in place. It determines how the part is located, where clamping forces are applied, and how much support the workpiece receives during cutting. These factors can influence repeatability, dimensional accuracy, vibration, and tool access throughout the machining process.
Fixture design becomes more important when a part has thin walls, irregular geometry, tight tolerances, or requires multiple setups. The workholding needs to provide enough rigidity to resist cutting forces without distorting the part or interfering with the tool path.
No Beska, fixture planning is considered together with part geometry, machining access, and inspection requirements before production begins. This helps identify potential workholding risks early and provides a more stable basis for machining.
2. Common Types of CNC Machining Fixtures
CNC machining fixtures range from simple standard workholding to dedicated systems built around a specific part. The right type depends on the workpiece geometry, the number of surfaces that need to be machined, the required repeatability, and how often the setup will be used.
Machine Vises and Soft Jaws
Machine vises are one of the most common workholding methods for prismatic parts. They are quick to set up, easy to adjust, and work well when the part has flat, accessible clamping surfaces.
Soft jaws extend the flexibility of a standard vise. The jaws can be machined to match the contour of the workpiece, providing better support and more consistent location than flat jaws alone. They are especially useful for parts with irregular profiles or finished surfaces that should not be marked by hard jaws.
Modular Fixtures
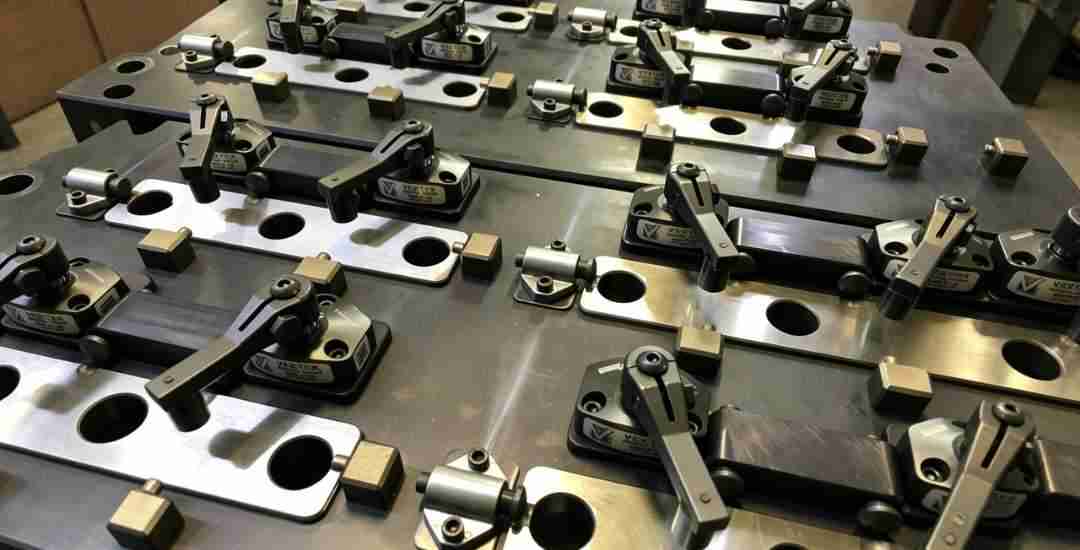
Modular fixtures are assembled from reusable components such as base plates, locating pins, stops, support blocks, and clamps. Their main advantage is flexibility because the same components can be rearranged for different parts or future design changes.
They are commonly used for prototypes, low-volume production, and part families where building a fully dedicated fixture would add unnecessary cost and preparation time. Their effectiveness still depends on proper support and locating, especially when cutting forces are high.
Dedicated Fixtures
A dedicated fixture is designed around the geometry and machining sequence of a particular part or part family. Locators, clamps, and supports are positioned specifically for the required operations, which can make loading more repeatable and reduce setup variation.
Dedicated fixtures are often considered when the same part is produced repeatedly, when standard workholding cannot provide enough access, or when several critical features need to maintain a consistent relationship across multiple operations.
Vacuum Fixtures
Vacuum fixtures hold the workpiece against a fixture plate using negative pressure rather than conventional mechanical clamps. This can provide clear access to the upper surface because there are fewer clamps around the cutting area.
They are commonly considered for flat or relatively thin parts where conventional clamping could obstruct machining or introduce local distortion. Their suitability depends on the available sealing area, surface condition, cutting forces, and how well the workpiece can maintain a vacuum seal.
Hydraulic and Pneumatic Fixtures
Hydraulic and pneumatic fixtures use powered clamping elements instead of manual clamps. They can apply clamping force in a controlled and repeatable way, which is useful when parts are loaded frequently or several clamps need to operate together.
Hydraulic systems are generally associated with higher clamping forces, while pneumatic systems are often used where faster, lighter clamping is sufficient. In both cases, the fixture still needs suitable locating and support so clamping force does not distort or shift the workpiece.
Indexing and Rotary Fixtures
Indexing and rotary fixtures allow the workpiece to be repositioned to a controlled angle without completely removing and relocating it. This can be useful for parts that require machining on several sides or at repeated angular positions.
Typical applications include housings, valve bodies, flanges, and components with equally spaced features. Repeatable indexing is important because any positioning error can transfer directly into the relationship between features machined at different orientations.
5-Axis Workholding Fixtures
Workholding for Usinagem de 5 eixos is usually designed to expose as much of the part as possible while keeping clamps and fixture bodies away from the tool, spindle, and rotary motion.
Low-profile fixtures, dovetail-style holding, compact vises, and custom fixture plates are often used to improve access around the workpiece. Fixture height and clamp position need to be considered together with the full machine motion so the part can tilt and rotate without creating interference.
For complex parts, 5-axis workholding can reduce the number of separate setups, but the fixture still needs to provide stable locating and enough rigidity for the planned cutting conditions.
3. How to Choose the Right CNC Fixture
The right fixture depends on how the part will be machined, how accurately it needs to be located, and how often the setup will be repeated. Part geometry, production volume, tolerance, material, and machining strategy are usually the main factors to consider.
Geometria parcial
Simple prismatic parts can often be held with a vise, soft jaws, or other standard workholding. Irregular surfaces, thin walls, or parts with limited clamping areas may require additional supports or a dedicated fixture that locates the workpiece from more suitable features.
Volume de produção
For prototypes and small batches, flexible workholding can reduce fixture preparation and make design changes easier to accommodate. As production volume increases, a dedicated fixture may become more useful when it shortens loading time, improves repeatable positioning, or supports multiple machining operations.
Tolerance Requirements
Tighter tolerances place more demand on locating accuracy, fixture rigidity, and clamping consistency. The fixture should hold the part securely without allowing cutting forces or clamping pressure to shift the workpiece away from its intended reference.
Workpiece Material
Material properties also affect workholding. Thin or relatively soft parts can deform when clamping force is too high, while harder materials and heavier cutting conditions may require greater support and rigidity.
The clamping method should therefore match both the material and the geometry of the part.
Estratégia de Usinagem
The fixture must also work with the planned machining operations. Multi-sided and 5-axis machining require enough clearance for the cutting tool, spindle, and rotary movement throughout the programmed toolpath.
Fixture height, clamp position, and accessibility should be considered before machining starts so the workholding does not block critical features.
4. Core CNC Fixture Design Principles
A fixture can only work well when the workpiece is located consistently, supported against cutting forces, and held without unnecessary distortion. Tool access and chip evacuation also need to be considered from the beginning, especially when several surfaces are machined in one setup.
Accurate Locating and Repeatability
The fixture should bring every workpiece back to the same machining reference. Locating pins, stops, and datum surfaces are commonly used to control the position of the part before clamping begins.
Repeatability becomes especially important when several parts are machined in sequence or when a component returns to the fixture for another operation. Worn or damaged locating surfaces can gradually affect positioning, so these features should remain accessible for inspection and maintenance.
Rigidity and Workpiece Support
The fixture and workpiece need enough rigidity to resist movement and vibration during cutting. Supports should be placed where they can help the part withstand machining forces without allowing unsupported sections to flex.
This becomes more important for thin walls, long features, or heavy roughing operations. Additional support may improve stability, but it should not interfere with the surfaces that need to be machined.
Controlled Clamping
Clamping force needs to hold the workpiece securely against its locating and support surfaces. Too little force can allow movement during machining, while excessive force can distort thin or flexible parts.
Clamp location also matters. Applying force close to supported areas generally creates a more stable setup than clamping an unsupported section of the workpiece.
Tool and Coolant Access
A fixture should secure the part without blocking the cutting tool, spindle, or coolant flow. Tall clamps, support blocks, and fixture walls can restrict access and force unnecessary changes to the machining strategy.
For complex setups, including the fixture model in toolpath simulation can help identify possible interference before machining begins.
Chip Evacuation
Chips should be able to leave the cutting area without becoming trapped between the workpiece and fixture. Accumulated chips can interfere with loading, locating, and coolant flow, especially during repeated production cycles.
Open spaces, clearance around locating features, and accessible cleaning areas can make the fixture easier to use and help maintain more consistent workholding from one part to the next.
5. Common Fixture Materials
Fixture materials need to provide enough rigidity and wear resistance for the machining process while remaining practical to manufacture, handle, and maintain. The best choice depends on whether the material is used for the main fixture body, a locating component, a clamp surface, or a protective contact point.
| Material | Características principais | Usos comuns |
| Liga de aço | High rigidity, good wear resistance, durable under repeated use | Fixture bodies, locating components, heavy-duty production fixtures |
| Aço para ferramentas | High hardness and wear resistance after heat treatment | Locating pins, bushings, clamp pads, and other wear-prone components |
| Alumínio | Lightweight, easy to machine, good stiffness-to-weight ratio | Prototype fixtures, low-volume fixtures, fixture plates, and lightweight workholding |
| Ferro fundido | Good rigidity and vibration damping | Heavy fixture bases and applications where vibration control is important |
| Aço inoxidável | Good corrosion resistance | Fixture components exposed to moisture, coolant, or corrosion-sensitive environments |
| Urethane and Engineering Plastics | Non-marring and slightly compliant | Soft contact points, protective inserts, seals, and surfaces that contact finished parts |
Steel is commonly used where rigidity, durability, and wear resistance are the main priorities. Aluminum is easier to machine and significantly lighter, which can make it useful for fixture plates, prototypes, and setups that need frequent handling. Cast iron is more suitable where a heavy, stable base and vibration damping are important.
Not every fixture needs to be made from a single material. A steel or aluminum fixture body may use hardened locating pins, replaceable wear components, and softer inserts where the fixture contacts a finished surface. Combining materials in this way allows the fixture to provide rigidity where it is needed while reducing wear or surface damage at critical contact points.
6. When Does a Custom Fixture Make Sense?
A custom fixture becomes useful when standard workholding can no longer provide the access, support, or repeatability required by the part. The decision is usually based on the machining difficulty and the amount of repeated setup work rather than on production volume alone.
When Standard Workholding Limits Machining
A vise, soft jaws, or modular setup may be sufficient for simple parts, but complex geometry can make standard workholding difficult to use. Parts with thin walls, irregular surfaces, limited clamping areas, or features on several sides may need a fixture designed around the actual machining sequence.
A custom fixture can provide support where it is needed while keeping critical surfaces accessible to the cutting tool.
When Repeatable Positioning Becomes Important
Dedicated locating features can be useful when the same part is loaded repeatedly or when several operations need to maintain a consistent relationship between machined features.
This becomes more important as tolerance requirements tighten or when setup variation begins to affect inspection and machining consistency.
When Setup Time Becomes a Production Constraint
For repeated production, the time required to locate, clamp, and verify each workpiece can become significant. A fixture designed for a specific part can simplify loading and reduce the number of manual adjustments required between cycles.
The benefit is usually greater when the same setup will be used regularly over a longer production run.
When the Fixture Investment Can Be Justified
A custom fixture adds design, machining, and validation work before production begins, so it is not automatically the best choice for every project. Its value should be weighed against the time spent on repeated setups, the risk of workpiece distortion or movement, and the difficulty of maintaining consistent positioning with standard workholding.
For simple prototypes or low-volume parts that can be held reliably with a vise or soft jaws, a dedicated fixture may add unnecessary work. For more demanding or repeated machining, however, the fixture can become an important part of the production strategy.
7. Fixture Selection Checklist
Before finalizing a CNC fixture, it is useful to check the setup as a complete system rather than evaluating the clamps or locating features separately. A fixture may look rigid and secure but still create problems if it blocks tool access, traps chips, or makes loading difficult.
The following checklist covers the main points to review before the fixture is released for production.
| Checkpoint | What to Check |
| Rigidez | Can the fixture and workpiece resist cutting forces without noticeable movement or vibration? |
| Locating | Are the datum surfaces, stops, and locating features able to position each workpiece consistently? |
| Clamping | Is the clamping force sufficient to hold the part securely without distorting thin or sensitive features? |
| Tool Access | Can the cutting tool and spindle reach all required features without interference from clamps or fixture components? |
| Compatibilidade de materiais | Are the fixture and contact materials suitable for the workpiece, especially where surface protection or wear resistance matters? |
| Chip and Coolant Flow | Can chips and coolant move away from the cutting area without collecting around locating or clamping points? |
| Loading and Unloading | Can the operator position and remove the part easily and consistently without unnecessary adjustment? |
A fixture does not need to be complex to be effective. The important point is that locating, clamping, support, access, and handling work together for the actual machining process. If one of these areas creates uncertainty, it is usually worth resolving before production begins.
Conclusão
The right CNC fixture depends on the geometry of the part, the machining operations, the required repeatability, and how often the setup will be used. Standard vises, modular systems, and dedicated fixtures can all work well when the locating, clamping, support, and tool access are matched to the actual machining requirements.
For CNC-machined parts, workholding should be considered before production starts rather than treated as a setup detail afterward. At Beska, fixture planning is reviewed together with part geometry, machining access, and critical dimensions so potential workholding issues can be identified before machining begins.
 Portuguese
 English
 Hebrew
 Turkish
 French
 Russian
 German
 Spanish