


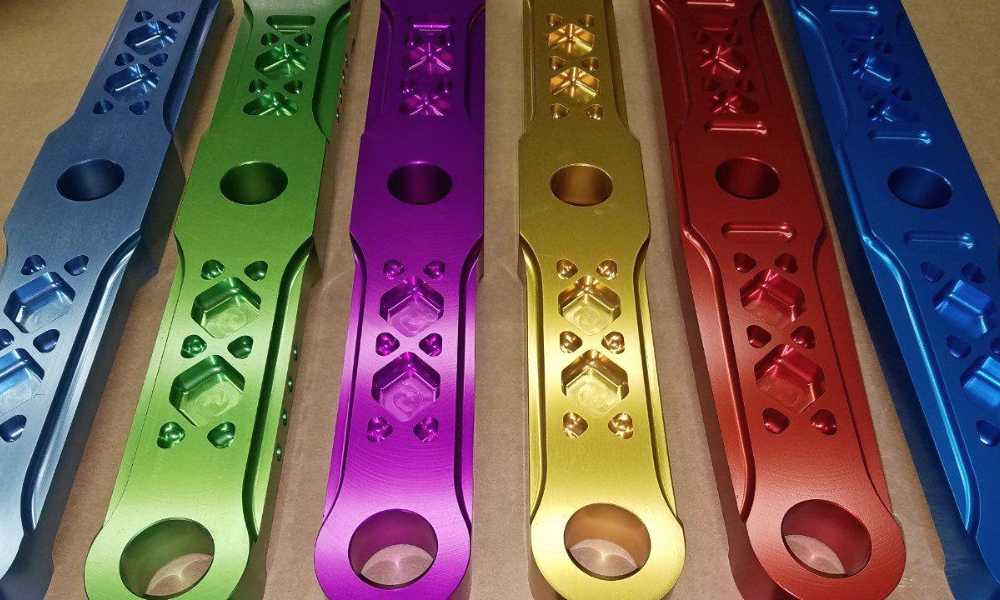
Anodizing is a widely used surface treatment in metal processing. It not only improves corrosion and wear resistance but also adds a variety of vibrant colors to metal parts. For CNC aluminum projects, selecting the right anodized color is essential to achieve both aesthetic appeal and functional performance.
The anodizing color chart provides a helpful reference, showing the range of shades metals can display under different anodizing conditions. But what determines these colors, and which finishes are best for your specific application? Our team can guide you through the options, and you can request samples to see the exact color and finish.
Keep reading to explore how anodizing works, key factors affecting colors, and the most common finishes used across industries.
1. How Anodizing Works: Basic Principles and Process
Anodizing is an electrochemical process that forms an oxide layer on the surface of a metal. Taking aluminum and its alloys as the most common example, when an aluminum part acts as the anode in a specific electrolyte solution, direct current is applied. Aluminum atoms lose electrons to become aluminum ions, which enter the electrolyte. Meanwhile, oxygen ions in the electrolyte move toward the anode and combine with the aluminum ions to form aluminum oxide. This oxide layer gradually builds up on the surface, creating a protective film with a specific thickness and structure.
The процесс анодирования generally involves four main steps:
- Pre-treatment: This essential cleaning phase removes oils, grease, dirt, and any existing oxides. A clean surface ensures the oxide layer forms uniformly and bonds well.
- Анодирование: Parameters such as electrolyte type, temperature, voltage, current density, and duration are carefully controlled. These factors influence the growth rate, thickness, and quality of the oxide film.
- Coloring: Depending on the desired finish, the oxide layer can be left natural or colored using various techniques, including integral coloring, dye absorption, or electrolytic coloring.
- Sealing: The porous oxide layer is sealed, often by hot water or chemical methods, to close pores, enhance corrosion resistance, and lock in color for long-term stability.
Each step will affect the durability, appearance, and performance of the final anodized part.

2. Key Factors Influencing Anodizing Colors
Anodizing colors depend on multiple interacting factors. These variables combine like pigments on a palette to create a wide range of hues.
Material Composition
Different metals and alloys produce different base colors after anodizing. For example, pure aluminum grades like 1050 and 1100 typically appear silver-white when anodized in sulfuric acid baths but take on gold to yellow-brown shades in oxalic acid baths. Aluminum-copper alloys such as 2017 and 2024 show gray-white in sulfuric acid and light brown to reddish-gray in oxalic acid. The presence of elements like copper shifts the color toward red tones, while magnesium tends to yield lighter yellowish hues.
Oxide Layer Thickness
The oxide film generally ranges from about 5 to 25 microns thick. A thicker oxide layer usually deepens the color, especially for natural (undyed) finishes, by increasing light absorption and altering the film’s optical properties.
Alloy Variations
Even alloys with similar base metals can exhibit different anodized colors. For example, anodized 6061 and 7075 aluminum may differ in tone and brightness due to differences in their chemical makeup and microstructure.
Coloring Time and Concentration
When dyes are used, the duration of immersion and the dye’s concentration both affect color depth and saturation. Longer exposure or higher dye concentration typically results in richer, more intense colors.
Sealing Process
Sealing—performed by hot water, chemical treatments, or other methods—closes the oxide pores and can subtly influence the final color. It also improves corrosion resistance and helps maintain color stability over time.
3. Anodizing Coloring Methods
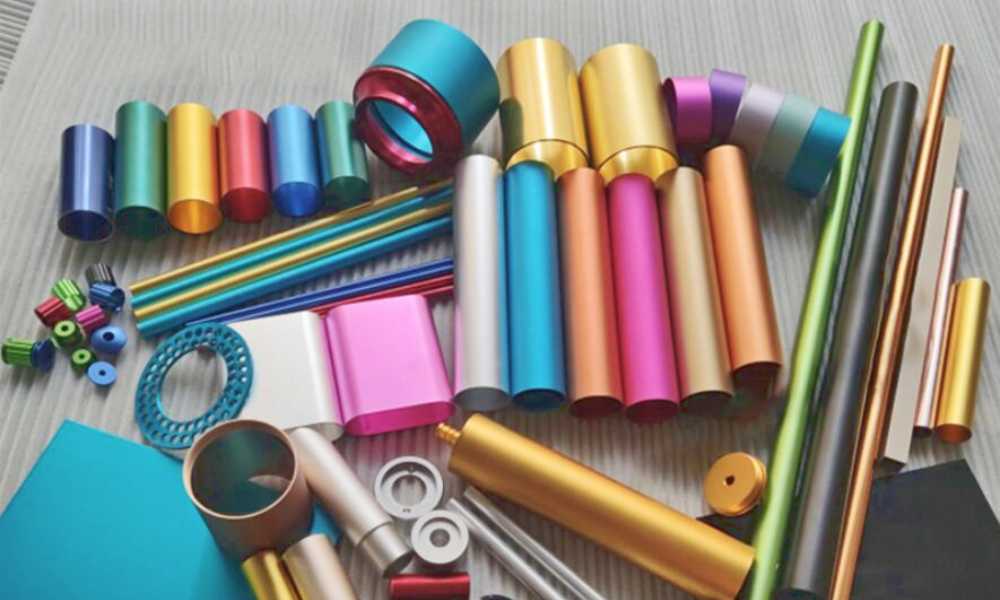
There are several coloring techniques used in anodizing, each producing distinct color effects:
Integral Coloring
This method controls electrolyte composition and process conditions during anodizing to produce natural colors in the oxide film. For example, oxalic acid baths can yield silver, brass, or brown shades, while chromic acid baths produce gray to dark gray tones, often called gunmetal gray. Integral colors are fused into the oxide layer, offering good weather resistance, though the color range is limited.
Dye Absorption Coloring
The most common method involves soaking the anodized part in organic or inorganic dye solutions. The porous oxide layer absorbs dye molecules, allowing a broad spectrum of colors. While vibrant, these colors may be less durable and offer reduced mechanical strength compared to integral colors.
Electrolytic Coloring
This technique deposits metal ions into the oxide pores during a secondary electrochemical process. The resulting colors fall between integral and dye colors in terms of range and durability. Electrolytic coloring often uses metal salts such as tin, nickel, cobalt, or mixtures to achieve specific shades and is well-suited for outdoor applications.
| Metal Salt Type | Typical Colors | Characteristics |
| Tin (Sn) | Champagne, Bronze | Most common, wide color range |
| Никель (Ni) | Black, Dark Brown | High weather resistance |
| Cobalt (Co) | Deep Blue, Black | Higher cost, special uses |
| Mixed Salts | Red Copper, Purple | Requires precise control |
4. International Standards for Anodizing Colors
Several widely recognized standards help define anodizing processes, color specifications, and performance requirements.
Pantone Color Matching
Some anodizing suppliers can customize finishes to match Pantone color codes. Pantone is a standardized color matching system extensively used in design, branding, and manufacturing. This allows anodized parts to precisely meet brand color requirements or aesthetic specifications.

RAL Color System
The RAL system is a popular European color standard used to specify paint and coatings, including anodized finishes. Common RAL colors used in anodizing include RAL 9005 (jet black) and RAL 1028 (melting yellow). This system helps manufacturers and customers communicate exact color expectations.
MIL-A-8625
This is a United States military specification that outlines types of anodizing for aluminum and aluminum alloys, detailing performance criteria such as corrosion resistance and hardness. It classifies anodizing into three types:
- Type I: Chromic acid anodizing, typically thin and used for aerospace components.
- Type II: Sulfuric acid anodizing, the most common type with medium thickness and good corrosion resistance.
- Type III: Hard anodizing, producing thick, wear-resistant coatings for heavy-duty applications.
Compliance with MIL-A-8625 ensures anodized parts meet strict durability and performance standards, especially in the defense and aerospace sectors.
5. Common Anodized Colors and Their Applications
Anodizing offers a broad palette of colors, each with unique characteristics and typical uses. Below is an overview of common color categories along with their typical shades and applications:
| Color Category | Typical Shades | Notes/Uses |
| Natural | Silver, Light Gray | Undyed oxide film, varies by thickness |
| Black | Matte Black, Pure Black | Most common, requires high-purity dyes to prevent fading |
| Gold | Champagne, Rose Gold | Decorative, mimics electroplated finishes |
| Reds | Bright Red, Burgundy | UV sensitive, requires stabilization |
| Blues | Sky Blue, Navy Blue | Inorganic dyes like cobalt salts enhance durability |
| Greens | Grass Green, Dark Green | Organic dyes, environmental regulations may apply |
| Purples/Pinks | Light Purple, Pink | Less common, used for customization |
| Browns/Coppers | Coffee Brown, Copper | Antique look, popular in vintage styles |
 Among these, black shades are particularly popular, ranging from deep AN01 (pure black) to metallic AN10 (black nickel). For example, “Space Black” (AN05), often seen in electronic products, is actually a very deep gray. This color is achieved through specialized electrolytic coloring, which produces a uniform finish with a premium feel.
Silver tones maintain the natural metallic look of aluminum while improving hardness and corrosion resistance. Variations include the bright AN101 (high gloss silver) and the matte AN120. In aerospace applications, thick micro-arc oxidation layers such as AN110 (50-100 μm) provide exceptional durability and insulation properties.
Gold anodizing colors are frequently used in luxury goods and architectural elements. They range from light champagne shades like AN201 to deep rose gold tones such as AN215. High-end watch cases often feature AN208 antique gold, which develops a unique patina over time, adding to their charm.
Colored anodizing, including reds, blues, and greens, is mainly achieved through dye absorption. For instance, AN301 cherry red meets automotive-grade standards for durability, while AN415 deep space blue is a signature color for Apple’s MacBook, created using advanced nano-dye technology for consistent and vibrant results.
6. Technical Comparison of Common Anodized Colors
Different anodized colors not only offer aesthetic variety but also come with varying physical properties and performance characteristics. The table below summarizes key technical parameters of common anodized colors:
| Цвет | Толщина оксида | Surface Texture | Коррозионная стойкость | Expected Lifespan | Typical Use Cases |
| Silver | 5 μm | Smooth, fine | Умеренный | 3-5 years | Indoor decor, temporary parts |
| Clear | 2 μm | Smooth, uniform | Высокий | 10+ years | Precision instruments, medical |
| Black | 10 μm | Rough, textured | Высокий | 10+ years | Automotive parts, outdoor frames |
| Orange | 20 μm | High gloss | Очень высокий | 20+ years | Marine equipment, high-temp parts |
| Gold | 12 μm | Metallic luster | Высокий | 15+ years | Luxury goods, electronics shells |
7. Common Issues and Solutions
Despite its many benefits, anodizing can sometimes present challenges that affect the final quality of the coating.
Uneven Coloring
Variations in electrolyte temperature can cause inconsistent film growth, leading to uneven color distribution. Maintaining the temperature within ±1°C and applying a pulsed current (around 50 Hz) helps improve the uniformity of the oxide layer.
Coating Peeling
Poor adhesion between the oxide film and the metal surface may result in peeling. Introducing sandblasting with 80-120 grit abrasives during pre-treatment raises the substrate roughness to Ra 1.6–3.2 μm, significantly enhancing coating adhesion.
Localized Corrosion
Areas with incomplete sealing are prone to corrosion. Using nickel salt sealing at 95°C and maintaining the bath pH between 5.5 and 6.5 achieves a sealing efficiency above 95%, providing robust corrosion resistance.
8. How CNC Machining Affects Anodizing Results
The way aluminum parts are machined can significantly influence the final anodized color, uniformity, and durability. Here are some key technical considerations:
- Surface Finish Matters: The metal’s surface roughness affects how anodizing absorbs dyes. Polished surfaces (Ra < 0.4 µm) generally produce brighter, reflective colors, while matte or bead-blasted finishes result in deeper, more uniform shades.
- Edge Geometry and Burrs: Sharp corners, tight grooves, or residual burrs from CNC operations can create uneven oxide layers or color pooling. Proper deburring and chamfering help ensure a consistent coating.
- Dimensional Stability: Anodizing adds a thin oxide layer (typically 5–25 µm), which can affect critical tolerances. Accounting for this during CNC machining helps maintain part fit and function.
- Material and Alloy Effects: Different aluminum alloys, such as 6061 and 7075, respond differently to anodizing. Alloy composition influences color saturation, brightness, and corrosion resistance, so selecting the right material is crucial for achieving the desired finish.
- Machining Planning: Aligning CNC tool paths and surface textures with anodizing requirements improves both visual quality and functional performance, minimizing post-processing issues.
By carefully combining CNC machining expertise with anodizing know-how, we ensure aluminum parts achieve consistent color, finish, and performance across a wide range of applications.
Заключение
Anodizing provides a practical and effective solution to enhance both the durability and appearance of metal parts. The final colors you see are the result of many factors from material selection to coloring techniques. By familiarizing yourself with these variables and consulting a detailed anodizing color chart, you can better specify finishes that meet both functional and aesthetic needs.
Whether you’re selecting coatings for industrial components, consumer electronics, or decorative elements, understanding anodizing options empowers you to make informed decisions. Ready to explore how anodizing can elevate your next CNC aluminum project? Dive deeper into the specifics or протянуть руку to an expert like the Beska team to find the perfect color and finish your application.
Погрузитесь глубже в наши ресурсы
Для вашего содержательного чтения мы составили список рекомендуемых статей:
- Anodizing Service
- Alodine vs Anodize
- What Is Passivation
- CNC Post-processing
- Услуги по обработке на станках с ЧПУ
 Russian
 English
 Hebrew
 Turkish
 French
 German
 Spanish
 Portuguese