


In sheet metal fabrication, poorly finished edges can lead to safety hazards, reduced structural integrity, and compromised aesthetics. This is where sheet metal hemming stands out. It ensures that metal edges are smooth, strong, and reliable.
Despite being a seemingly minor step, hemming affects not only product durability and safety but also assembly precision and visual quality. For engineers and manufacturers, questions such as “Which hemming method best suits my material?” or “How can I prevent edge cracking or deformation?” are common concerns.
In this article, we will explore the purpose, types, techniques, and applications of sheet metal hemming.
1. Что такое кромкование листового металла?

Sheet metal hemming refers to the process of folding or treating the edges of metal sheets to remove sharp corners, improve strength, and enhance appearance. After cutting, stamping, or laser processing, the edges often have burrs or rough surfaces that can cause injuries, lead to cracks, or affect visual quality. Hemming smooths and reinforces these edges using mechanical, thermal, or adhesive methods.
Technically, the process may include deburring, chamfering, polishing, and edge strengthening. It is not merely making the edges smooth but a precise engineering step that combines materials science, mechanical strength, and design accuracy. A well-executed hemming process improves the product’s quality, safety, and overall aesthetics.
2. The Purpose of Sheet Metal Hemming
Skipping the hemming process may save time, but it can lead to safety hazards, deformation, or poor appearance. The value of hemming can be seen in four main areas.
Safety Protection
After cutting, materials such as stainless steel or cold-rolled steel often have sharp edges or burrs. Hemming, for example by folding or wrapping, transforms these edges into smooth, safe surfaces and prevents injuries during handling or use.
Structural Reinforcement
Thin or irregular sheet metal structures frequently experience stress concentration at the edges. Hemming connects and strengthens these edges, increasing rigidity and resistance to deformation, which is crucial for thin-walled or high-stress components.
Sealing and Dust Prevention
In enclosures for electronics, vehicles, or medical devices, unsealed edges can allow dust, moisture, or oil to enter. Hemming, whether through welding or adhesive bonding, provides effective sealing and improves product reliability and longevity.
Aesthetic Improvement
For visible sheet metal parts such as furniture frames or appliance panels, edge quality directly affects visual appeal. Hemming ensures uniform color, clean lines, and a professional finish that enhances the perceived value of the product.
In short, hemming is not just a finishing step. It safeguards users, reinforces structure, protects against contamination, and enhances the overall appearance, making it an essential part of high-quality sheet metal fabrication.
3. Types of Sheet Metal Hemming
Hemming methods can be classified by process type and material type, each suited to different production requirements.
3.1 Process-Based Classification
Bending Hemming

It is a cost-effective and simple method that uses a press brake to fold the sheet edge inward or outward, typically forming a 90° double-layered edge. This method requires no additional material, keeps costs low, and allows fast processing. It is commonly used for cabinets, covers, trays, and protective enclosures. However, it is less suitable for thick plates above 3 mm or for curved and irregular shapes.
Welding Hemming

It achieves high strength and reliable sealing by closing edges through TIG, spot, or laser welding. This method is ideal for heavy-duty components such as machinery housings, automotive parts, and medical frames. While it provides excellent structural reinforcement, it is labor-intensive, requires skilled welders, and may introduce heat-affected zones that need subsequent finishing.
Adhesive Hemming
It uses bonding agents like structural glue, hot-melt adhesives, or tapes to attach sealing strips to the edges. It is highly flexible, suitable for curved shapes, and prevents deformation of thin sheets. This method is commonly applied in appliances, furniture, and electronic enclosures. Its main limitation is that adhesive strength may degrade under prolonged exposure to high temperatures or humidity.
Roll Hemming
It relies on rollers to fold or attach the sheet edges automatically, offering high consistency and precision. It is especially suited for mass production of components like car doors, sinks, HVAC panels, and containers. While this automated method improves uniformity and efficiency, it requires higher equipment investment and is less economical for very small batches.
These four hemming methods provide a range of solutions for different structural requirements, production volumes, and aesthetic needs.
3.2 Material-Based Classification
Hemming can also be categorized according to the material of the edge treatment. The table below summarizes the main types, their advantages, limitations, and typical applications:
| Тип материала | Common Examples | Преимущества | Ограничения | Типичные применения |
| Metal Hemming | Stainless steel, aluminum, galvanized steel | High strength, excellent durability | Heavier, higher cost | Industrial equipment, outdoor enclosures |
| Non-Metal Hemming | PVC, ABS, rubber, wood strips | Lightweight, colorful, easy to shape | Lower strength, aging risk | Furniture, consumer electronics |
| Composite Hemming | Metal-plastic or metal-rubber combination | Combines strength and flexibility | Costly, complex fabrication | Automotive seals, premium appliances |
Hemming material selection further refines the process to meet specific performance, appearance, and durability requirements.
4. Key Differences: Hemming vs Seaming vs Bending
When forming metal edges, engineers often need to decide between hemming, seaming, and bending. Each method offers distinct advantages depending on strength, material, and cost considerations. The comparison below clarifies their main differences:
| Метод | Описание процесса | Structural Strength | Suitable Materials | Cost Consideration |
| Подшивание | Folds or treats edges to remove sharp corners and reinforce strength; may include welding or adhesive | Высокий | Aluminum, stainless steel, cold-rolled steel | Higher, requires precise tooling and control |
| Закрытие швов | Interlocks two metal edges to create a secure joint | Середина | Thin panels, lightweight metals | Moderate, simpler than hemming |
| Изгиб | Alters metal angle along a fold line without additional edge treatment | Низкий | Thin sheets, low-stress metals | Low, fast and economical |
Knowing these differences helps select the most suitable edge-forming method for each application. Hemming is ideal for visible or load-bearing edges, seaming works for panel joining, and bending is best for simple, low-stress folds.
5. Applications of Hemming in Modern Manufacturing
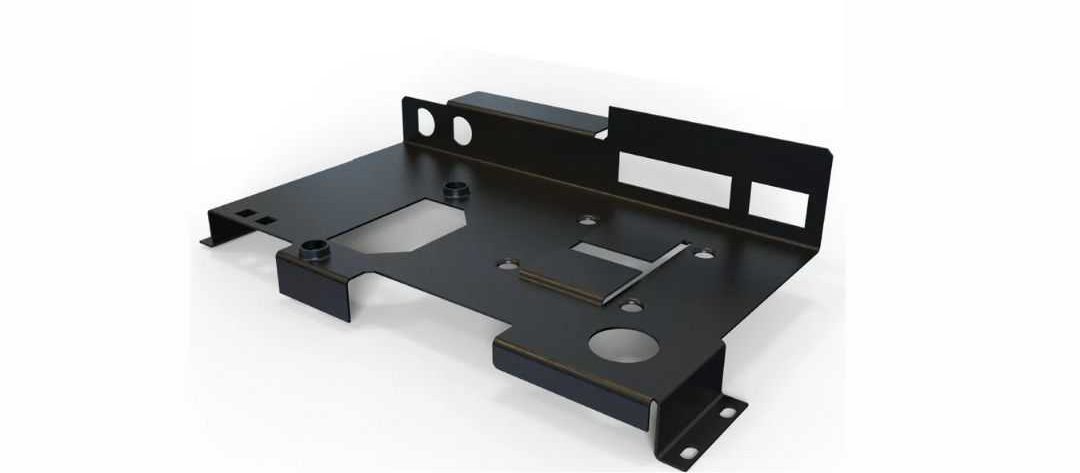
Sheet metal hemming is widely used across industries to enhance the safety, strength, and appearance of metal components. Its versatility makes it a key process in modern manufacturing.
Автомобильная промышленность
Hemming is applied to car doors, engine hoods, tailgates, and other panels. It smooths edges, reduces assembly hazards, and reinforces structural integrity while improving the visual finish of exterior components.
Consumer Electronics, Appliances, and Furniture
Hemming ensures safe, durable, and visually appealing edges for appliance enclosures, electronic devices, and metal furniture. Panels of washing machines, refrigerators, and shelving units benefit from reinforced edges and better assembly alignment.
Универсальность материала
Hemming works with aluminum, stainless steel, and cold-rolled steel, allowing manufacturers to balance strength, weight, and corrosion resistance without compromising edge quality.
Overall, hemming not only protects users but also enhances product durability and appearance across diverse applications.
6. Technical Considerations in Sheet Metal Hemming
Achieving high-quality hemming goes beyond selecting the right method and material. Several technical factors directly affect the final edge performance and appearance.
Radius and Angle Control
Precision hemming requires careful control of edge radius and bending angle. Different applications demand specific curvatures. Handheld devices benefit from softer, rounded edges for comfort, while assembly interfaces require tighter angles to ensure proper alignment. Controlling these parameters is essential to meet both functional and aesthetic requirements.
Свойства материала
Each metal behaves differently during hemming. Aluminum is soft and prone to burrs, stainless steel is harder and requires higher forming force, and copper can deform if overworked. Understanding these characteristics is critical to selecting the right hemming approach and ensuring consistent quality across production runs.
Process Order
The sequence of operations in sheet metal fabrication can significantly impact hemming results. Typically, hemming is performed after forming but before surface finishing to ensure smooth coating and a uniform appearance. For complex components, multiple hemming steps may be required to achieve the desired edge geometry.
Проверка качества
A reliable hemming process includes systematic inspection to maintain quality. Manufacturers often conduct visual and tactile checks for burrs, precise dimensional measurements, and durability testing under stress or vibration. These measures help ensure that the final product meets both functional and aesthetic standards.
Paying attention to these technical considerations ensures that the hemming process consistently delivers safe, strong, and visually refined edges.
7. Common Hemming Defects and Their Causes
No hemming process is entirely immune to issues. Certain problems tend to appear repeatedly, depending on the method and materials used.
| Проблема | Распространенные причины | Примечания |
| Cracking | Excess bending angle, incompatible welding material, excessive heat | Common in welding or bending hemming |
| Edge Lifting | Insufficient adhesive pressure, uneven glue, roller misalignment | Seen in adhesive and roll hemming |
| Poor Sealing | Welding pores, incomplete bonding, material mismatch | Affects dust- or water-tight performance |
| Surface Defects | Scratches, burn marks, residue, discoloration | Often due to poor post-processing |
| Dimensional Error | Machine misalignment, rebound deformation | Impacts assembly precision |
Addressing these issues carefully ensures that the final product is safe, durable, and visually consistent.
Заключение
Sheet metal hemming may be a subtle process, but it reflects a manufacturer’s craftsmanship and attention to detail. It safeguards both functionality and aesthetics, demonstrating the balance between engineering precision and design quality. From the smooth edges of a car door to the seamless frame of a home appliance, every perfect finish starts with a reliable hemming process.
Consulting an experienced supplier like the Beska team who ensures consistent quality, material versatility, and precision control, helping your sheet metal forming projects achieve both safety and premium appearance.
Погрузитесь глубже в наши ресурсы
Для вашего содержательного чтения мы составили список рекомендуемых статей:
- Sheet Metal Bending Process
- Sheet Metal Punching Process
- Sheet Metal Assembly Techniques
- Sheet Metal Forming Service
 Russian
 English
 Hebrew
 Turkish
 French
 German
 Spanish
 Portuguese